Executive Summary
A nutraceutical manufacturer required an extraction facility to produce premium-quality Ashwagandha extract standardised to 5% Withanolides for domestic and international markets. The customer sought a complete turnkey solution capable of maintaining pharmaceutical-grade quality while minimising solvent consumption, reducing operating costs, and maximising extraction efficiency.
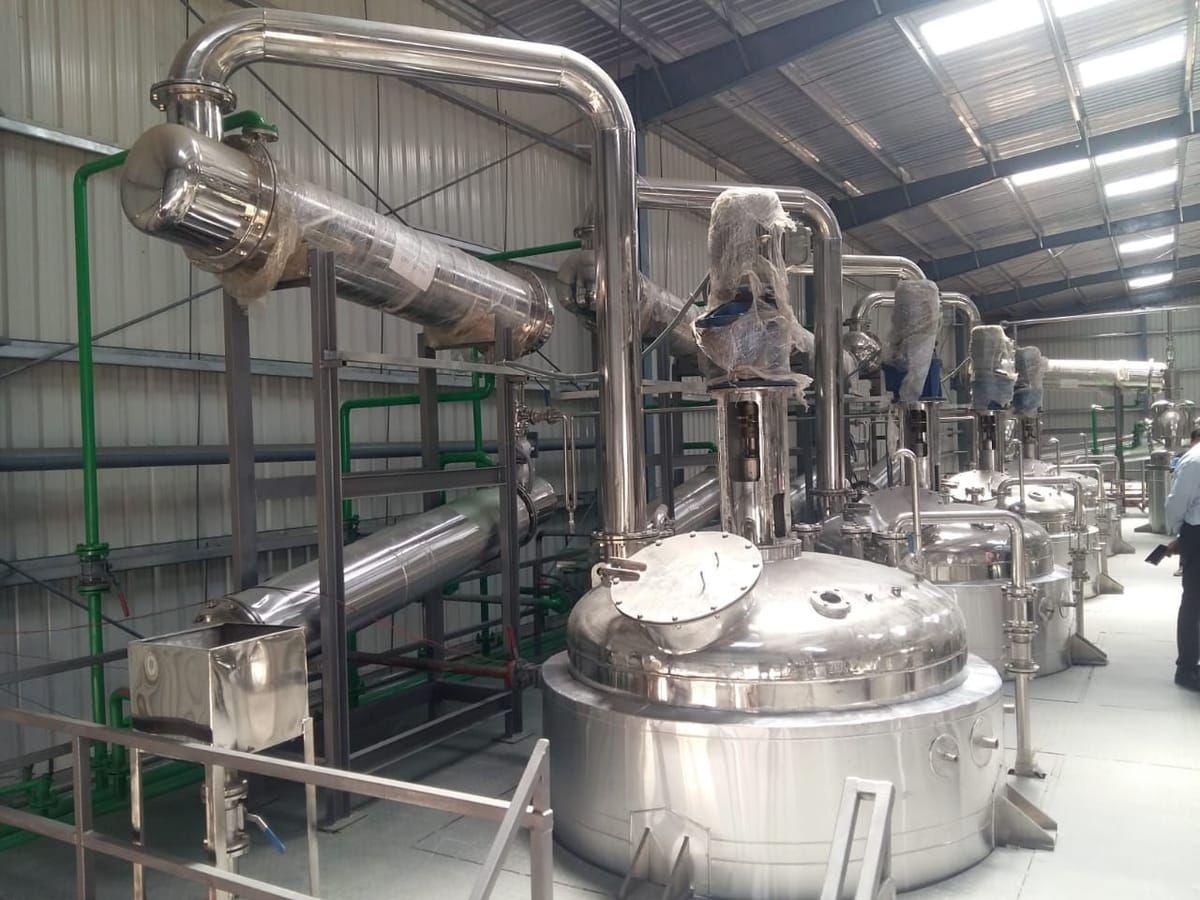
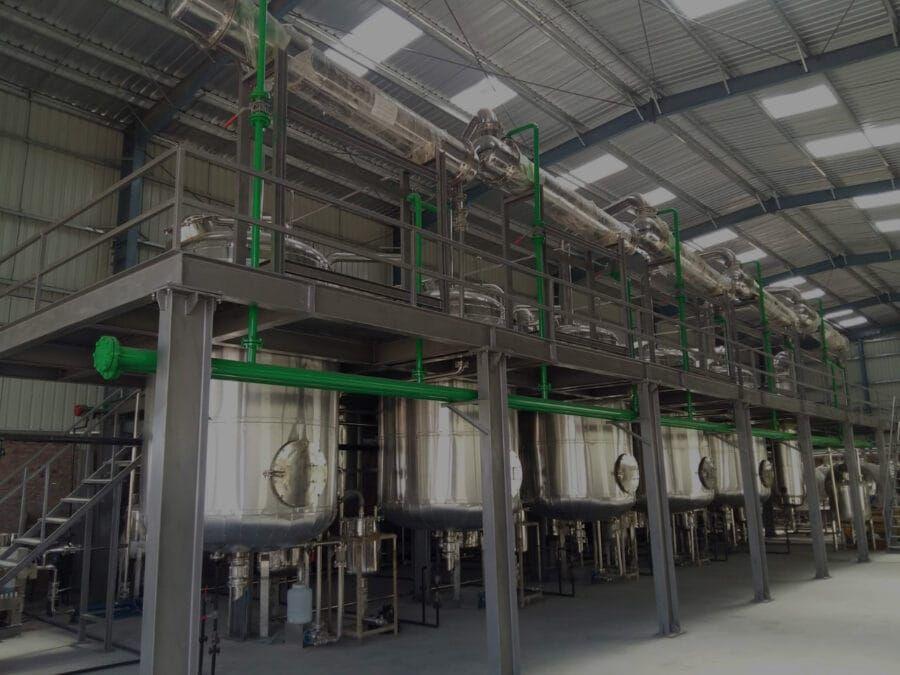
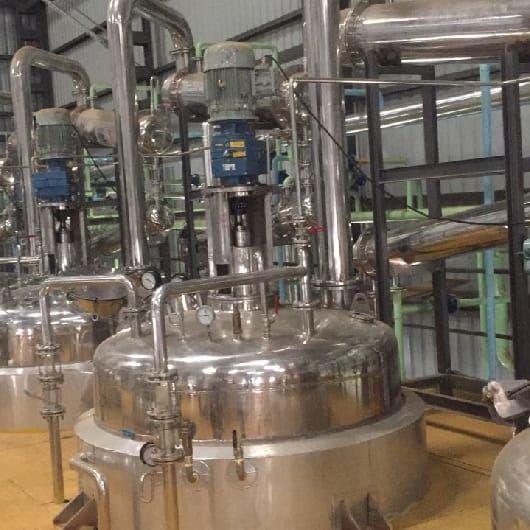
Mechotech engineered, manufactured, installed, and commissioned a fully integrated Ashwagandha Extraction Plant featuring automated extraction, vacuum concentration, solvent recovery, filtration, drying, and clean-in-place (CIP) systems.
Customer Challenges
The client faced several production and quality challenges:
- Low extraction efficiency using conventional extraction systems
- High ethanol consumption
- Significant solvent losses
- Inconsistent Withanolide content
- Manual operations leading to batch variations
- High steam consumption
- Long production cycles
- Difficulty meeting export quality standards
- Limited production capacity
- Need for GMP-oriented equipment
Project Objectives
Mechotech was entrusted with delivering a complete turnkey extraction facility capable of:
- Processing 5 Tons of Ashwagandha roots per day
- Producing pharmaceutical-grade extract
- Achieving maximum Withanolide recovery
- Reducing operating costs
- Minimising solvent losses
- Maintaining closed-loop solvent handling
- Fully complying with GMP requirements
- Enabling future capacity expansion
Raw Material
- Botanical Name
- Withania somnifera
- Common Name
- Ashwagandha
- Plant Part Used
- Roots
- Incoming Moisture
- 8–12%
- Raw Material Size
- 10–20 mm after milling
- Daily Capacity
- 5,000 kg/day
Process Flow
Process Description
Raw Material Preparation
Cleaned Ashwagandha roots are mechanically reduced to the optimum particle size to maximise extraction efficiency while maintaining good solvent permeability.
Extraction
The prepared botanical material is transferred into stainless steel extraction vessels where controlled hydro-alcoholic extraction is carried out under optimised temperature conditions.
The automated extraction cycle ensures:
- Minimal degradation
- Uniform batch quality
- Reduced extraction time
Solid-Liquid Separation
The extract slurry passes through precision filtration systems designed to achieve excellent clarification while minimising product losses.
Vacuum Concentration
The filtered extract enters a multi-stage vacuum evaporator where ethanol is gently removed under reduced pressure.
Benefits include:
- Preservation of heat-sensitive compounds
- Reduced steam consumption
- Improved product quality
- Higher concentration efficiency
Solvent Recovery
One of the major highlights of the plant is its high-efficiency solvent recovery system.
Recovered ethanol is:
- Purified
- Condensed
- Recycled back into production
This significantly reduces solvent purchase costs and environmental impact.
Drying
The concentrated extract is dried using suitable drying technology selected according to customer specifications, such as vacuum tray drying or spray drying.
The resulting powder exhibits:
- Low residual moisture
- High stability
- Uniform particle size
Standardisation
Final extract batches are standardised to customer specifications, including:
- 2.5% Withanolides
- 5% Withanolides
- 10% Withanolides
Major Equipment Supplied
- Raw Material Cleaning System
- Hammer Mill
- Stainless Steel Extraction Vessels
- Solvent Storage Tanks
- Solvent Transfer Pumps
- Plate Heat Exchangers
- Pressure Leaf Filter
- Vacuum Evaporator
- Solvent Recovery System
- Condensers
- Vacuum Pumps
- Vacuum Tray Dryer / Spray Dryer Interface
- CIP System
- Storage Tanks
- Finished Product Tanks
- PLC-Based Control Panel
- Electrical MCC
- Instrumentation System
Automation Features
The plant incorporates advanced PLC-SCADA automation for:
- Recipe management
- Batch control
- Temperature monitoring
- Vacuum control
- Solvent level monitoring
- Alarm management
- Historical data logging
- Production reporting
- Energy monitoring
- Remote diagnostics
GMP & Safety Features
The facility is designed with hygienic, GMP-oriented practice in view; the standards that apply to the client's facility and product are scoped per project. Key features include:
- SS 316L product contact parts
- Hygienic piping
- Sanitary valves
- CIP compatibility
- Flameproof electrical components in solvent areas
- Nitrogen blanketing
- Explosion-proof design where required
- Earthing and bonding
- Safety interlocks
- Pressure relief systems
Plant Utilities
- Steam Boiler
- Chilled Water System
- Cooling Tower
- Air Compressor
- Vacuum System
- Electrical Power
- Soft Water
- Nitrogen Supply
Customer Benefits
Following commissioning, the customer experienced:
- Increased extraction yield
- Consistent Withanolide standardisation
- Lower ethanol consumption
- Reduced production costs
- Improved batch reproducibility
- Faster production cycles
- Reduced manpower
- Enhanced operator safety
- Export-ready product quality
Plants Used In This Project
Why Mechotech?
Mechotech provides comprehensive turnkey solutions for herbal extraction facilities, integrating advanced process engineering, energy-efficient technologies, GMP-oriented manufacturing, and intelligent automation. Withexpertise in botanical extraction systems, the company delivers reliable, scalable, and customised plants for nutraceutical, pharmaceutical, food, and cosmetic industries worldwide.
Conclusion
This Ashwagandha Extraction Plant demonstrates Mechotech's ability to deliver turnkey herbal extraction solutions that combine operational efficiency and documentation support. By integrating advanced solvent recovery, precision process control, and hygienic design, the plant enables manufacturers to produce high-value Ashwagandha extracts with confidence and supporting sustainable production.
Planning a Similar Plant?
Mechotech engineers are ready to assess your process and design the right plant for your target output.
Get a Free Consultation