Supercritical CO₂ (SCFE) Extraction Plant
Supercritical CO₂ (SCFE) Extraction Plant
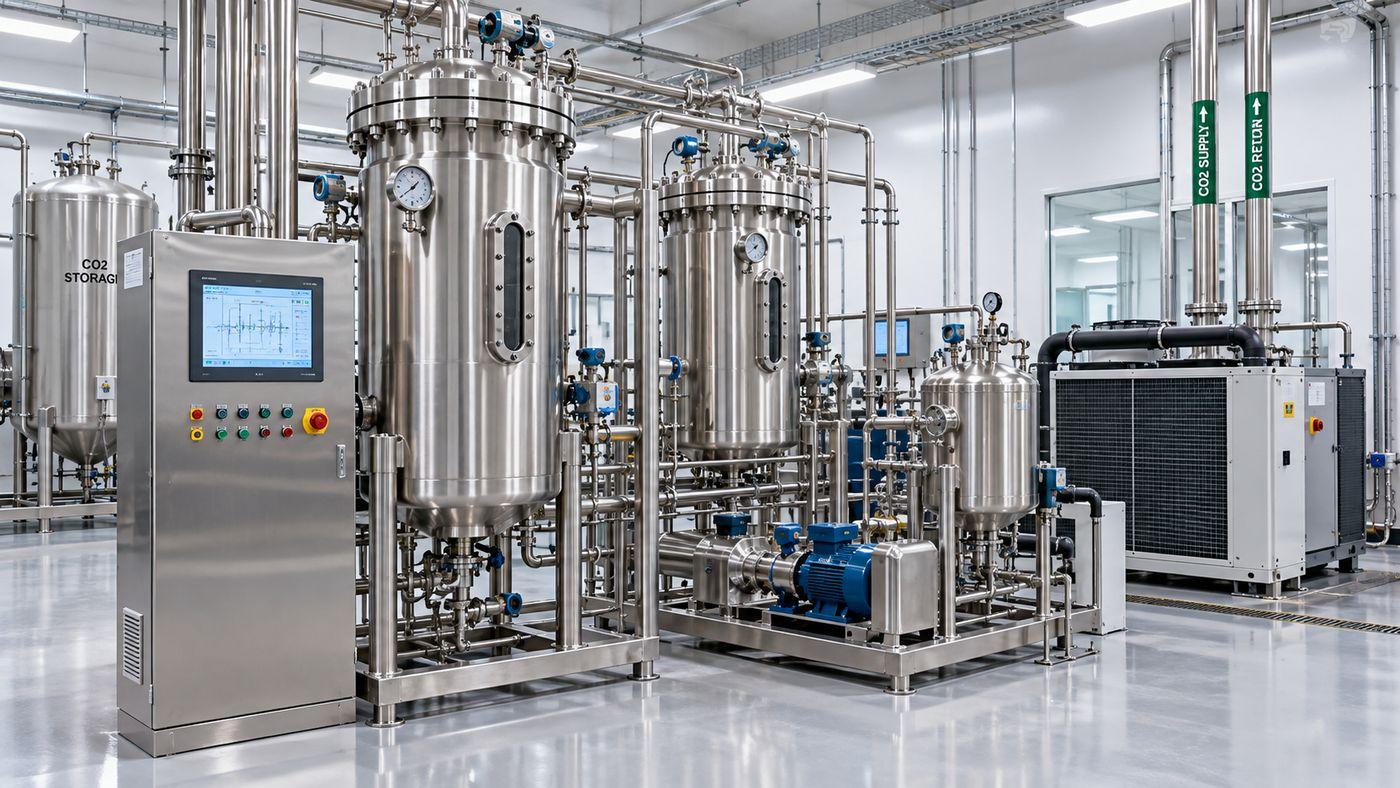
Mechotech designs and manufactures turnkey supercritical CO₂ (SCFE) extraction plants that use carbon dioxide above its critical point as a clean, tunable, solvent-free extraction medium. Supercritical CO₂ combines gas-like penetration with liquid-like solvent power, so it dissolves target compounds from a botanical bed at low temperature and then releases them completely when the pressure is dropped — leaving a residue-free, high-purity extract. Mechotech engineers the complete system — extraction vessels, fractional separators, high-pressure CO₂ pump, co-solvent dosing, chilling, CO₂ recovery and PLC-SCADA controls — for the nutraceutical, pharmaceutical, food, flavour, fragrance and cosmetic industries.
A Mechotech SCFE plant is built around a high-pressure extraction vessel (or a bank of vessels) served by a ceramic-plunger CO₂ high-pressure pump, a refrigerated chiller that liquefies the CO₂, and precise extractor/separator heat exchangers that hold each stage at its set temperature. Extract selectivity is tuned by adjusting pressure and temperature, and an optional food-grade ethanol co-solvent (entrainer) extends recovery to more polar compounds. Laden CO₂ is expanded across one or more separators so fractions drop out stage by stage, then the CO₂ is recompressed and returned to storage by a closed-loop recovery system for economical, low-emission operation. Product-contact parts are built in stainless steel 304, with safety valves and software overpressure protection throughout; capacity, vessel count and automation level are configured to the customer's feedstock, throughput and product mix.
Process Flow
Technical Specifications
| Technology | Supercritical Fluid Extraction (SCFE / supercritical CO₂) |
|---|---|
| Working Principle | CO₂ above its critical point as a tunable, solvent-free extraction fluid |
| Extraction Vessel | Configured to requirement — pilot to multi-vessel industrial |
| Separators | One- or two-stage fractional separation (configurable) |
| Extraction Pressure | Up to ~40–50 MPa design (configured to process requirement) |
| Separation Pressure | ~20–25 MPa (configurable) |
| Operating Temperature | Ambient to ~85 °C (configurable) |
| Co-Solvent / Entrainer | Food-grade ethanol (optional, for polar compounds) |
| CO₂ Handling | Closed-loop recovery, recompression and recycle |
| Product-contact Material | Stainless steel 304 |
| Automation | PLC / SCADA with touchscreen (configurable) |
| Utilities | Refrigerated chiller / cooling, electrical power, food-grade CO₂ |
| Safety | Safety valves on all pressure vessels + software overpressure alarms |
| Output | Solvent-free extract, essential oil, oleoresin or isolate |
Plant Capacities
| Plant Size | Scale / Usage | Configuration | Design Pressure | Operating Temperature |
|---|---|---|---|---|
| 1 L | Pilot / R&D | Single vessel | up to ~50 MPa | ambient–85 °C |
| 2 L | Pilot / R&D | Single vessel | up to ~50 MPa | ambient–85 °C |
| 5 L | Pilot / R&D | Single vessel | up to ~50 MPa | ambient–85 °C |
| 10 L | Lab / small production | Twin vessel | up to ~50 MPa | ambient–85 °C |
| 20 L | Lab / small production | Twin vessel | up to ~40 MPa | ambient–85 °C |
| 30 L | Small production | Twin vessel | up to ~40 MPa | ambient–85 °C |
| 50 L | Production | Twin vessel | up to ~40 MPa | ambient–85 °C |
| 100 L | Production | Multi-vessel | up to ~40 MPa | ambient–85 °C |
| 200 L | Commercial | Multi-vessel | up to ~40 MPa | ambient–85 °C |
| 300 L | Commercial | Multi-vessel | up to ~40 MPa | ambient–85 °C |
| 500 L | Commercial | Multi-vessel | up to ~40 MPa | ambient–85 °C |
| 1000 L | Industrial | Multi-vessel train | up to ~40 MPa | ambient–85 °C |
| 2000 L | Industrial | Multi-vessel train | up to ~40 MPa | ambient–85 °C |
| 3000 L+ | Industrial (large) | Multi-vessel train | up to ~40 MPa | ambient–85 °C |
Standard SCFE plant sizes; separators, CO₂ high-pressure & co-solvent pumps, chiller, CO₂ recovery, SS 304 construction and PLC-SCADA controls are scaled to each plant. Every size is configured to the customer's feedstock and throughput — larger and custom capacities on request.
Manufacturing Process
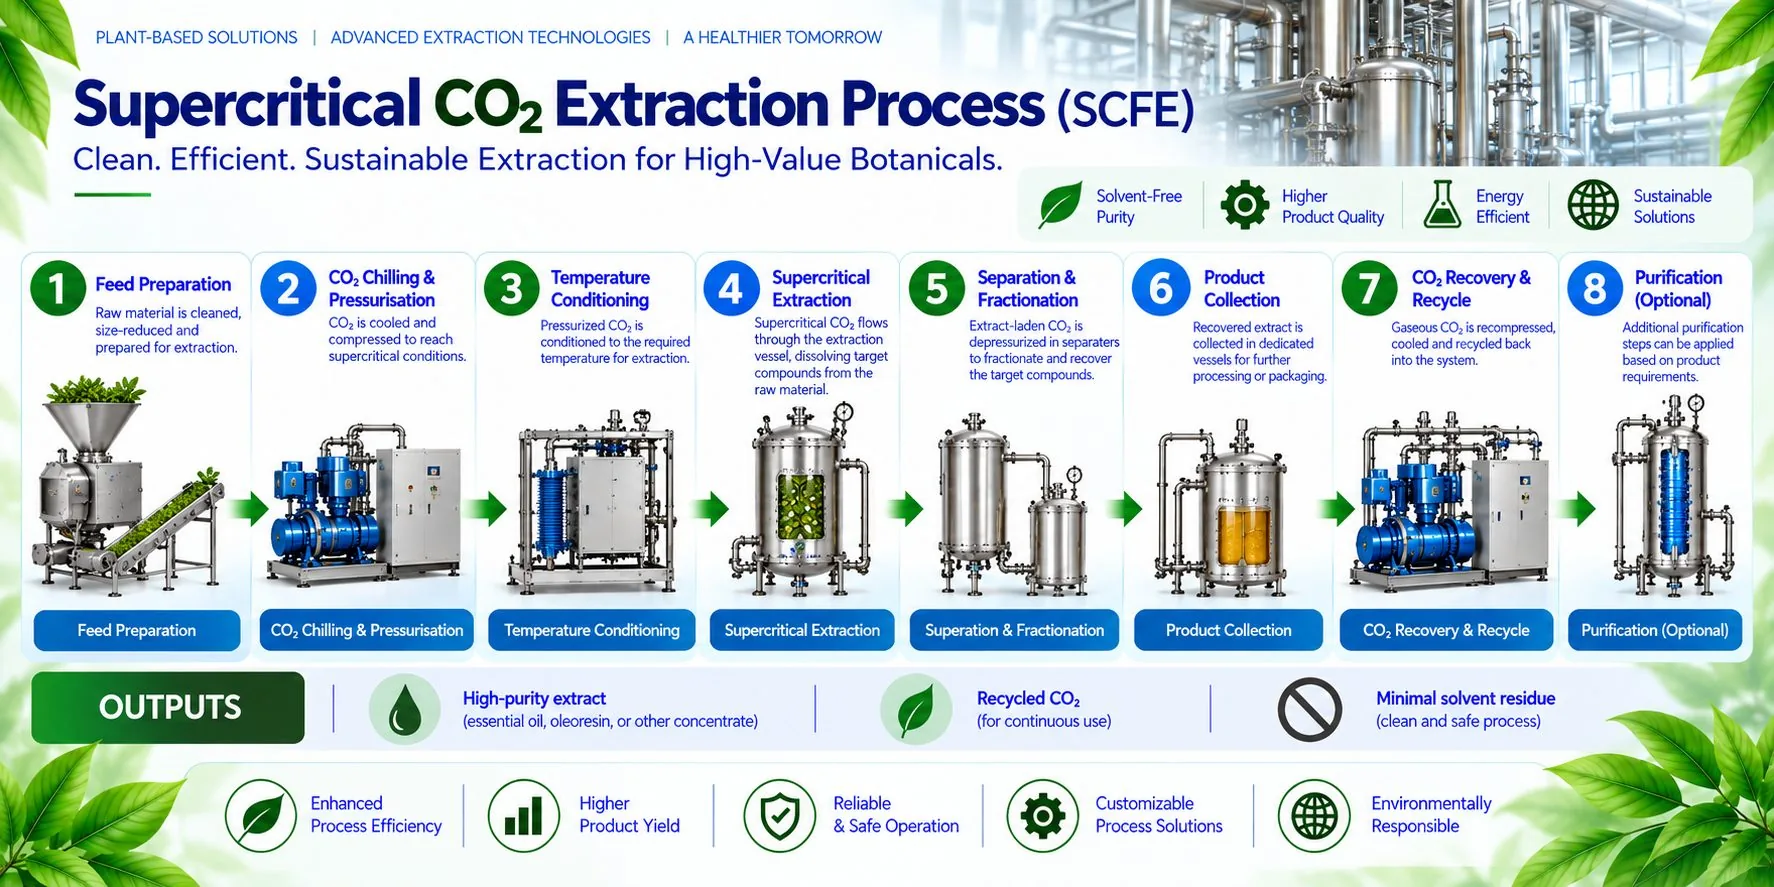
Feed Preparation
The botanical raw material is cleaned, dried and milled to an optimal particle size so supercritical CO₂ can penetrate the bed evenly and contact the target compounds.
CO₂ Chilling & Pressurisation
Food-grade CO₂ is liquefied in a refrigerated chiller and raised by the high-pressure pump above its critical point (about 31 °C and 7.4 MPa) into the supercritical state.
Temperature Conditioning
The extractor heat exchanger brings the supercritical CO₂ to the set extraction temperature, fixing the fluid's density and therefore its dissolving power.
Supercritical Extraction
Supercritical CO₂ percolates the packed extraction vessel, dissolving the target solutes; an optional ethanol co-solvent can be dosed in to recover more polar actives.
Separation & Fractionation
The laden CO₂ is expanded across one or more separators; stepwise reductions in pressure and temperature precipitate the extract, allowing fractions to be collected separately.
Product Collection
The solvent-free extract, essential oil or oleoresin is drawn from the separator vessels — multiple separators enable fractional collection of distinct quality cuts.
CO₂ Recovery & Recycle
The now-clean CO₂ is recompressed and recondensed by the closed-loop recovery system and returned to the storage tank for reuse, cutting operating cost and emissions.
Purification (Optional)
The extract can be winterised and short-path/molecular distilled on matched downstream equipment to reach isolate or crystal-grade purity.
Applications
- Essential oils and aroma extracts (e.g. agarwood/oud, ginger, nutmeg, rosemary, lavender, vanilla)
- Spice oleoresins (black pepper, cinnamon, turmeric, chilli)
- Coffee and tea decaffeination
- Resins and gums (frankincense, myrrh)
- Hops and botanical bitters extraction
- Carotenoids and antioxidants (lycopene, astaxanthin, seabuckthorn actives)
- Alkaloids, flavonoids and saponins from herbal medicine
- Nutraceutical, pharmaceutical, food, flavour, fragrance and cosmetic ingredient production
Key Features
Solvent-Free, Residue-Free Extract
CO₂ leaves no solvent residue — when the pressure drops it simply gasses off, giving a clean extract ideal for food, nutraceutical and pharmaceutical use.
Tunable Selectivity
Adjusting pressure and temperature changes CO₂ density and dissolving power, so the same plant can target different compounds and quality fractions.
Low-Temperature Processing
Extraction runs at mild temperatures that protect heat-sensitive aromas, actives and colours from thermal degradation.
Closed-Loop CO₂ Recovery
An integrated recovery and recycle loop reclaims the CO₂ each cycle for economical, low-emission operation.
Optional Co-Solvent & Fractional Separators
A food-grade ethanol entrainer extends recovery to polar compounds, while multiple separators allow fractional collection of distinct cuts.
SS 304 Build, PLC-SCADA & Full Safety
Stainless-steel product-contact construction, recipe-based PLC/SCADA control, and safety valves with software overpressure protection throughout.
Frequently Asked Questions
What is supercritical CO₂ (SCFE) extraction?
How does a supercritical CO₂ extraction plant work?
Why choose SCFE over conventional solvent extraction?
What can a supercritical CO₂ plant extract?
What capacity and pressure are available?
Is the CO₂ recovered and reused?
Does Mechotech supply the plant turnkey?
Does Mechotech offer CO2 extraction plants for specific botanicals?
Ready to discuss your project?
Get a free quote and technical consultation from our engineering team.