Executive Summary
A manufacturer of botanical active ingredients required a fully integrated extraction facility for the production of pharmaceutical-grade Berberine Hydrochloride (HCl) derived from botanical sources such as Berberis aristata and Coscinium fenestratum. The primary objective was to achieve high product purity while minimising solvent consumption, reducing operating costs, and ensuring consistent batch quality for export markets.
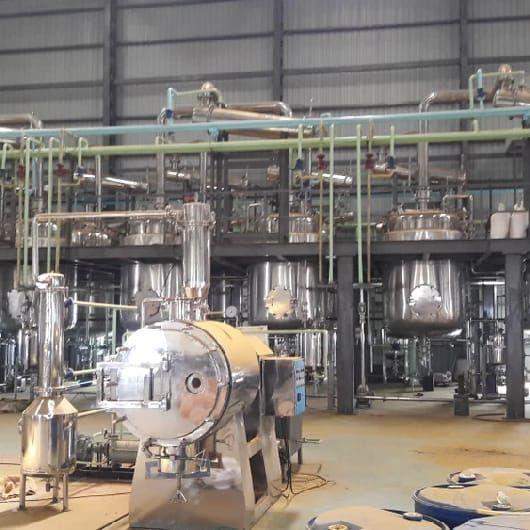
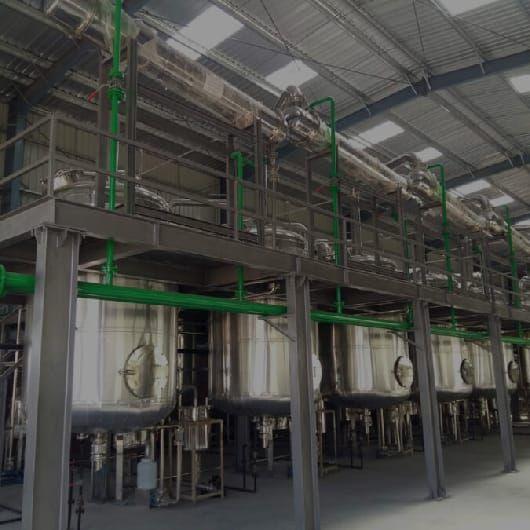
Mechotech designed and supplied a turnkey Berberine HCl Extraction Plant, incorporating advanced extraction, purification, pH-controlled conversion, crystallisation, filtration, drying, solvent recovery, and PLC-SCADA automation.
Customer Background
The customer is a producer of botanical extracts supplying ingredients to pharmaceutical companies, dietary supplement manufacturers, and international herbal product brands. Growing demand for Berberine HCl required expansion from semi-manual production to a modern automated facility capable of meeting stringent quality and regulatory standards.
Customer Challenges
Before implementing the new plant, the customer faced several issues:
- Low Berberine recovery from botanical raw materials
- High solvent consumption
- Manual pH adjustment causing inconsistent product quality
- Long batch processing times
- Difficult purification procedures
- High labour requirements
- Variable crystal quality
- Poor solvent recovery
- Difficulty meeting export specifications
Project Objectives
The customer required a plant capable of:
- Processing 5 MT/day of botanical raw material
- Producing 97–98% Berberine Hydrochloride
- Maximising alkaloid recovery
- Closed-loop solvent recovery
- Reducing utility consumption
- Automating critical processing stages
- Meeting GMP requirements
- Supporting future expansion
Raw Material
- Primary Botanical Sources
- Berberis aristata, Coscinium fenestratum, Phellodendron amurense
- Plant Part Used
- Stem, Bark, Root
- Daily Capacity
- 5,000 kg/day
Finished Product
Available Options
Applications
- Anti-diabetic formulations
- Nutraceutical capsules
- Herbal tablets
- Functional foods
- Pharmaceutical intermediates
Process Flow
Process Description
Raw Material Preparation
Botanical raw material is cleaned and milled to an optimised particle size, ensuring efficient solvent penetration and alkaloid extraction.
Solvent Extraction
The prepared material is loaded into stainless steel extractors, where food- or pharmaceutical-grade solvents are circulated under controlled temperature and agitation.
The optimised extraction cycle provides:
- High alkaloid recovery
- Uniform extraction
- Reduced solvent usage
- Improved productivity
Filtration
The extract is clarified using pressure leaf and polishing filters to remove suspended solids before concentration.
Vacuum Concentration
Clarified extract is concentrated under vacuum to preserve heat-sensitive alkaloids while recovering valuable solvent for reuse.
Benefits include:
- Lower steam consumption
- Better product stability
- Designed for efficient operation
- Improved downstream processing
Purification
The concentrated extract undergoes purification to remove pigments, tannins, and other unwanted constituents, producing a cleaner alkaloid-rich solution.
Berberine Hydrochloride Conversion
A precisely controlled pH adjustment converts purified Berberine into its hydrochloride salt, improving stability, purity, and pharmaceutical suitability.
Automated dosing systems ensure:
- Accurate reagent addition
- Controlled reaction conditions
- Batch consistency
- Reduced operator intervention
Crystallisation
Controlled cooling and agitation promote the formation of uniform Berberine HCl crystals with excellent purity and particle characteristics.
Centrifugation
High-speed centrifuges separate crystals from the mother liquor with minimal product loss.
Drying
Vacuum tray dryers reduce moisture while maintaining crystal integrity and chemical stability.
Final product characteristics include:
- Moisture below specification
- High purity
- Long shelf life
Pulverising & Blending
Dried crystals are milled and blended to achieve customer-specific particle size distribution before packaging.
Major Equipment Supplied
- Raw Material Cleaning System
- Hammer Mill
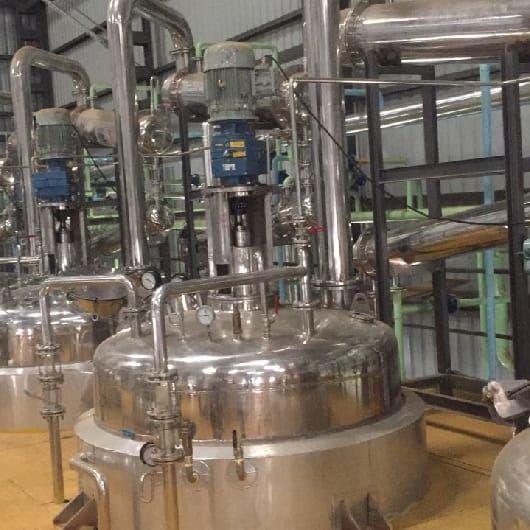
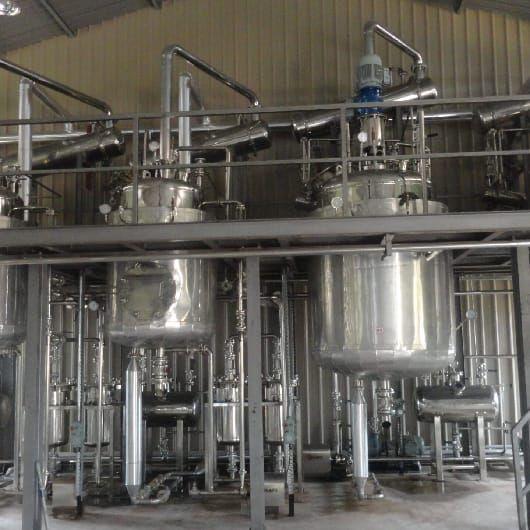
- Stainless Steel Extraction Vessels
- Solvent Storage Tanks
- Extraction Pumps
- Pressure Leaf Filters
- Cartridge Filtration System
- Vacuum Evaporator
- Purification Tanks
- Reaction Vessels
- Crystallisers
- Industrial Centrifuges
- Vacuum Tray Dryer
- Pulveriser
- Ribbon Blender
- Solvent Recovery Unit
- Condensers
- CIP System
- PLC-SCADA Control Panel
- Electrical MCC
- Instrumentation Package
Automation Features
The plant includes advanced PLC-SCADA automation with:
- Recipe management
- Automated extraction cycles
- pH-controlled reagent dosing
- Temperature and pressure monitoring
- Crystallisation profile control
- Batch recording
- Alarm management
- Production reporting
- Utility monitoring
- Remote diagnostics
GMP & Safety Features
Designed for pharmaceutical-grade manufacturing, the facility incorporates:
- SS 316L product-contact surfaces
- Hygienic piping and sanitary valves
- Closed-loop solvent handling
- Flameproof electrical equipment
- Nitrogen blanketing
- Pressure relief systems
- Emergency shutdown interlocks
- CIP-compatible design
- Validation-friendly construction
- Compliance with GMP and international safety practices
Plant Utilities
- Steam Boiler
- Cooling Tower
- Chilled Water System
- Vacuum System
- Air Compressor
- Electrical Power Supply
- Soft Water
- Nitrogen Supply
Customer Benefits
After commissioning the new facility, the customer achieved:
- Consistent production of pharmaceutical-grade Berberine HCl
- Closed-loop solvent recovery
- Reduced steam and utility consumption
- Lower labour costs through automation
- Shorter batch cycles
- Improved crystal quality
- Documentation to support regulatory qualification
- Lower overall manufacturing cost
Plants Used In This Project
Why Mechotech?
Mechotech is a manufacturer of turnkey extraction and processing plants for the nutraceutical, pharmaceutical, herbal, food, and specialty chemical industries. Our expertise includes advanced solvent extraction, purification, crystallisation, solvent recovery, automation, and GMP-oriented engineering. Every plant is customised to meet customer-specific product requirements, capacities, and international quality expectations.
Conclusion
The Berberine Hydrochloride Extraction Plant developed by Mechotech demonstrates how advanced engineering can transform botanical raw materials into high-value pharmaceutical ingredients. By integrating efficient extraction, precision purification, intelligent automation, and sustainable solvent recovery, the facility combines these process stages in a single turnkey solution.
Key Technical Highlights
- Raw Material
- Berberis aristata, Coscinium fenestratum, Phellodendron amurense
- Final Product
- Berberine HCl (97–98%)
- Solvent Recovery
- Established during process development
- Automation
- PLC-SCADA
- Construction
- SS 304 / SS 316L
- Compliance
- Hygienic, GMP-oriented design with documentation to support the client's qualification; applicable standards are scoped per project
- Applications
- Pharmaceuticals, Nutraceuticals, Herbal APIs, Functional Foods
Planning a Similar Plant?
Mechotech engineers are ready to assess your process and design the right plant for your target output.
Get a Free Consultation