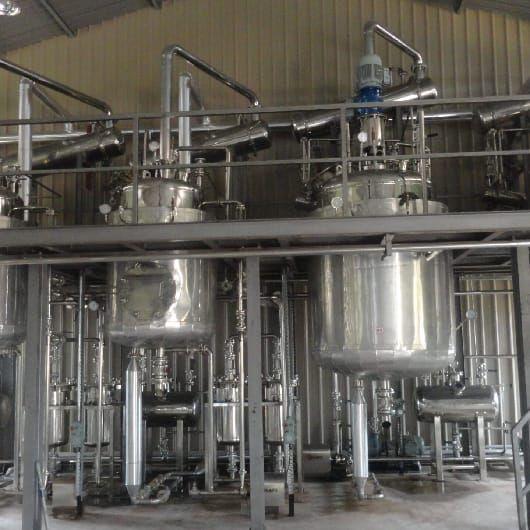
Executive Summary
A specialty chemical manufacturer required a fully automated, GMP-oriented and industrial-grade Gum Rosin & Turpentine Processing Plant to manufacture premium Gum Rosin, Gum Turpentine Oil (GTO), and value-added resin derivatives from natural pine oleoresin.
The customer required a turnkey processing facility capable of maximising gum rosin recovery, producing high-purity gum turpentine oil, minimising thermal degradation, reducing utility consumption, and consistently manufacturing export-grade products meeting international quality standards.
Mechotech successfully designed, engineered, manufactured, supplied, installed, and commissioned a Gum Rosin Processing Plant integrating advanced oleoresin melting, filtration, vacuum distillation, turpentine recovery, resin purification, automatic packing, and intelligent PLC-SCADA automation.
Customer Background
The customer manufactures specialty resin products for adhesive manufacturers, paint & coating companies, printing ink manufacturers, rubber processing industries, paper & packaging industries, pharmaceutical companies, fragrance manufacturers, and chemical exporters. Increasing worldwide demand for high-quality natural resins required investment in a modern automated processing facility with international manufacturing standards.
Customer Challenges
Before modernisation, the customer experienced:
- Poor gum rosin colour
- High turpentine losses
- High fuel consumption
- Manual production inconsistencies
- Long processing cycles
- Oxidation of resin
- High operating costs
- Limited production capacity
- Difficulty maintaining export quality
Project Objectives
Mechotech developed a turnkey solution capable of:
- Processing 50 MT/day of Pine Oleoresin
- Producing premium Gum Rosin
- Recovering high-purity Gum Turpentine Oil
- Minimising oxidation
- Reducing utility consumption
- Improving product consistency
- Meeting international quality standards
- Supporting expansion
Raw Material
- Source
- Natural Pine Oleoresin
- Botanical Species
- Pinus roxburghii, Pinus elliottii, Pinus merkusii, and other commercial pine species
- Raw Material Form
- Crude Gum Oleoresin
- Daily Processing Capacity
- 50,000 kg/day
Finished Product
Available Options
Applications
- Hot Melt Adhesives
- Pressure Sensitive Adhesives
- Paints & Coatings
- Printing Inks
- Rubber Compounding
- Paper Sizing
- Fragrance Chemicals
- Pharmaceutical Applications
Process Flow
Process Description
Raw Material Preparation
Crude pine oleoresin is received, inspected, and melted in jacketed stainless steel melting vessels under carefully controlled temperature conditions to prevent degradation.
Filtration
The molten oleoresin passes through multiple filtration stages to remove:
- Bark particles
- Dirt
- Sand
- Wood fibres
- Mechanical impurities
The filtration process significantly improves final gum rosin quality.
Vacuum Distillation
Filtered oleoresin enters specially designed vacuum distillation columns where volatile gum turpentine oil is separated from non-volatile gum rosin.
The process provides:
- Low thermal degradation
- Reduced oxidation
- Energy-efficient operation
Gum Turpentine Recovery
Recovered vapours are condensed using high-efficiency condensers to obtain premium Gum Turpentine Oil suitable for industrial and fragrance applications.
Rosin Purification
Remaining molten rosin undergoes polishing filtration before final storage and packing.
The purification system ensures:
- Better colour stability
- Low ash content
Automatic Packing
The finished gum rosin is packed into:
- Steel Drums
- Fibre Drums
- HDPE Bags
- Jumbo Bags
- Customised Export Packaging
Quality Standardisation
Gum Rosin:
- Colour Grade (WW, WG, X)
- Acid Value
- Softening Point
- Ash Content
- Unsaponifiable Matter
- Moisture
- Insoluble Matter
Gum Turpentine Oil:
- Alpha Pinene
- Beta Pinene
- Specific Gravity
- Refractive Index
- Distillation Range
- Colour
- Purity
Major Equipment Supplied
- Oleoresin Melting Tanks
- Heating System
- Coarse Filters
- Pressure Leaf Filters
- Vacuum Distillation Column
- Reboiler
- High-Efficiency Condensers
- Turpentine Storage Tanks
- Gum Rosin Storage Tanks
- Final Filtration Unit
- Automatic Filling Machine
- Drum Handling System
- PLC-SCADA Automation Panel
- Electrical MCC
- Instrumentation Package
- CIP System (where applicable)
Automation Features
The plant incorporates advanced PLC-SCADA automation featuring:
- Automatic Temperature Control
- Vacuum Control
- Distillation Sequence Management
- Product Level Monitoring
- Flow Monitoring
- Utility Monitoring
- Alarm Management
- Historical Batch Records
- Production Analytics
- Remote Diagnostics
- Energy Monitoring
- Industry 4.0 Connectivity
GMP & Safety Features
The plant incorporates international industrial safety standards. Features include:
- SS 316L / Carbon Steel construction (application dependent)
- Closed-loop vapour recovery
- Explosion-proof electrical systems
- Nitrogen blanketing
- Flameproof instrumentation
- Pressure safety valves
- Emergency shutdown system
- Fire protection integration
- Automated process interlocks
- Environmental compliance
Plant Utilities
- Thermic Fluid Heater
- Steam Boiler (Optional)
- Cooling Tower
- Vacuum System
- Air Compressor
- Electrical Power
- Nitrogen System
- Instrument Air
Sustainability Features
The plant incorporates sustainable engineering practices through:
- Energy-efficient vacuum distillation
- Heat recovery systems
- Closed-loop vapour recovery
- Low-emission operation
- Utility optimisation
- Reduced product losses
- Automated process control
- Environmentally responsible manufacturing
Customer Benefits
Following successful commissioning, the customer achieved:
- Higher gum rosin recovery
- Increased gum turpentine yield
- Reduced oxidation losses
- Lower utility costs
- Increased production capacity
- Improved product consistency
- Better export acceptance
- Enhanced operational safety
Plants Used In This Project
Why Mechotech?
Mechotech is a manufacturer of turnkey processing plants for natural resins, botanical extracts, essential oils, nutraceuticals, pharmaceuticals, specialty chemicals, and food processing industries. With engineering excellence, our expertise in vacuum distillation, resin purification, solvent recovery, intelligent PLC-SCADA automation, and industrial process engineering enables customers worldwide to manufacture premium resin products.
Conclusion
The Gum Rosin & Turpentine Processing Plant from Mechotech provides a complete turnkey solution for manufacturing premium Gum Rosin and Gum Turpentine Oil with excellent colour and high recovery efficiency. Through advanced vacuum distillation technology, intelligent automation, sustainable engineering, and robust industrial design, the facility combines these process stages in a single turnkey solution.
Key Technical Highlights
- Raw Material
- Natural Pine Oleoresin
- Finished Products
- Gum Rosin, Gum Turpentine Oil, Modified Rosin Products
- Technology
- Vacuum Distillation + Resin Purification + Vapour Recovery
- Automation
- PLC-SCADA with Industry 4.0 Integration
- Construction Material
- SS 304, SS 316L, Carbon Steel (application-specific)
- Compliance
- Hygienic, GMP-oriented design with documentation to support the client's qualification; applicable standards are scoped per project
- Applications
- Adhesives, Paints & Coatings, Printing Inks, Rubber, Paper, Pharmaceuticals, Fragrance Chemicals
Why Global Manufacturers Choose Mechotech
- engineering expertise in extraction, distillation, and specialty chemical processing
- Complete turnkey project execution from process design to commissioning
- Customised plants from pilot units to industrial facilities
- High-efficiency vacuum distillation with optimised energy consumption
- Intelligent PLC-SCADA automation with real-time monitoring and complete batch traceability
- Advanced vapour recovery and environmentally responsible process design
- Comprehensive installation, validation, operator training, preventive maintenance, spare parts support, and lifetime technical assistance
- Proven expertise in natural resins, essential oils, herbal extracts, oleoresins, nutraceuticals, pharmaceuticals, and specialty chemical processing plants
Planning a Similar Plant?
Mechotech engineers are ready to assess your process and design the right plant for your target output.
Get a Free Consultation