Executive Summary
A renowned international fragrance manufacturer required a fully automated, GMP-oriented Tuberose Absolute Extraction Plant capable of producing premium Tuberose Absolute, Tuberose Concrete, and high-value natural fragrance ingredients for luxury perfumes, cosmetics, personal care products, aromatherapy, and pharmaceutical applications.
Tuberose (Polianthes tuberosa, now classified as Agave amica) is one of the world's most valuable fragrance flowers. Due to its extremely delicate floral aroma, steam distillation is unsuitable for preserving its complete fragrance profile. Therefore, Mechotech designed a sophisticated closed-loop solvent extraction process with advanced vacuum solvent recovery and low-temperature purification.
Customer Background
The customer supplies fragrance ingredients to International Luxury Perfume Houses, Cosmetic Manufacturers, Premium Personal Care Brands, Aromatherapy Companies, Pharmaceutical Manufacturers, Fine Fragrance Houses, Incense Manufacturers, and Global Botanical Extract Exporters. The rapidly growing demand for premium natural floral fragrances encouraged investment in a fully automated, GMP-oriented extraction facility.
Customer Challenges
Prior to modernisation, the customer experienced:
- Low fragrance extraction efficiency
- Loss of delicate aromatic compounds
- High solvent consumption
- Manual process inconsistencies
- Variable fragrance quality
- High production costs
- Limited production capacity
- Difficulty meeting luxury export standards
- Safety concerns with solvent handling
Project Objectives
Mechotech developed a turnkey solution capable of:
- Processing 12 MT/day of Fresh Tuberose Flowers
- Producing premium Tuberose Concrete
- Producing export-grade Tuberose Absolute
- Achieving closed-loop solvent recovery
- Maximising fragrance preservation
- Reducing operating costs
- Meeting GMP, HACCP, and international fragrance standards
- Supporting future expansion
Raw Material
- Botanical Name
- Agave amica (Synonym: Polianthes tuberosa)
- Common Name
- Tuberose
- Plant Part Used
- Fresh Flowers
- Major Aromatic Components
- Methyl Benzoate, Benzyl Alcohol, Benzyl Benzoate, Farnesol, Eugenol, Nerolidol, Indole, Methyl Anthranilate
- Daily Processing Capacity
- 12,000 kg/day
Finished Product
Available Options
Applications
- Luxury Perfumes
- Fine Fragrances
- Premium Cosmetics
- Skin Care Products
- Aromatherapy
- Incense
- Personal Care Products
- High-End Toiletries
Process Flow
Process Description
Fresh Flower Handling
Fresh tuberose flowers are processed immediately after harvesting to preserve their highly volatile fragrance molecules.
A hygienic, low-impact conveying system minimises physical damage and aroma loss.
Closed-Loop Solvent Extraction
Prepared flowers are processed inside stainless steel extraction vessels using food-grade hydrocarbon solvent.
The solvent selectively dissolves aromatic compounds while maintaining the flower's natural fragrance profile.
Advantages include:
- Low solvent consumption
- Uniform extraction
Vacuum Solvent Recovery
The extract is transferred to vacuum evaporators where solvent is recovered under controlled low-temperature conditions.
Recovered solvent is automatically recycled into the extraction process.
Solvent is recovered for reuse.
Concrete Production
Following solvent removal, concentrated aromatic material forms premium Tuberose Concrete, containing natural waxes, pigments, and aromatic compounds.
Ethanol Purification
Concrete is dissolved in food-grade ethanol and chilled to sub-zero temperatures.
Natural waxes crystallise and are removed through precision filtration.
Vacuum Ethanol Recovery
Ethanol is recovered under vacuum, leaving behind highly concentrated Tuberose Absolute.
Quality Standardisation
Every production batch undergoes comprehensive laboratory analysis for:
- Methyl Benzoate
- Benzyl Alcohol
- Farnesol
- Indole
- Residual Solvent
- Specific Gravity
- Refractive Index
- Colour
- Aroma Profile
- GC-MS Fingerprint
Major Equipment Supplied
- Fresh Flower Conveyor
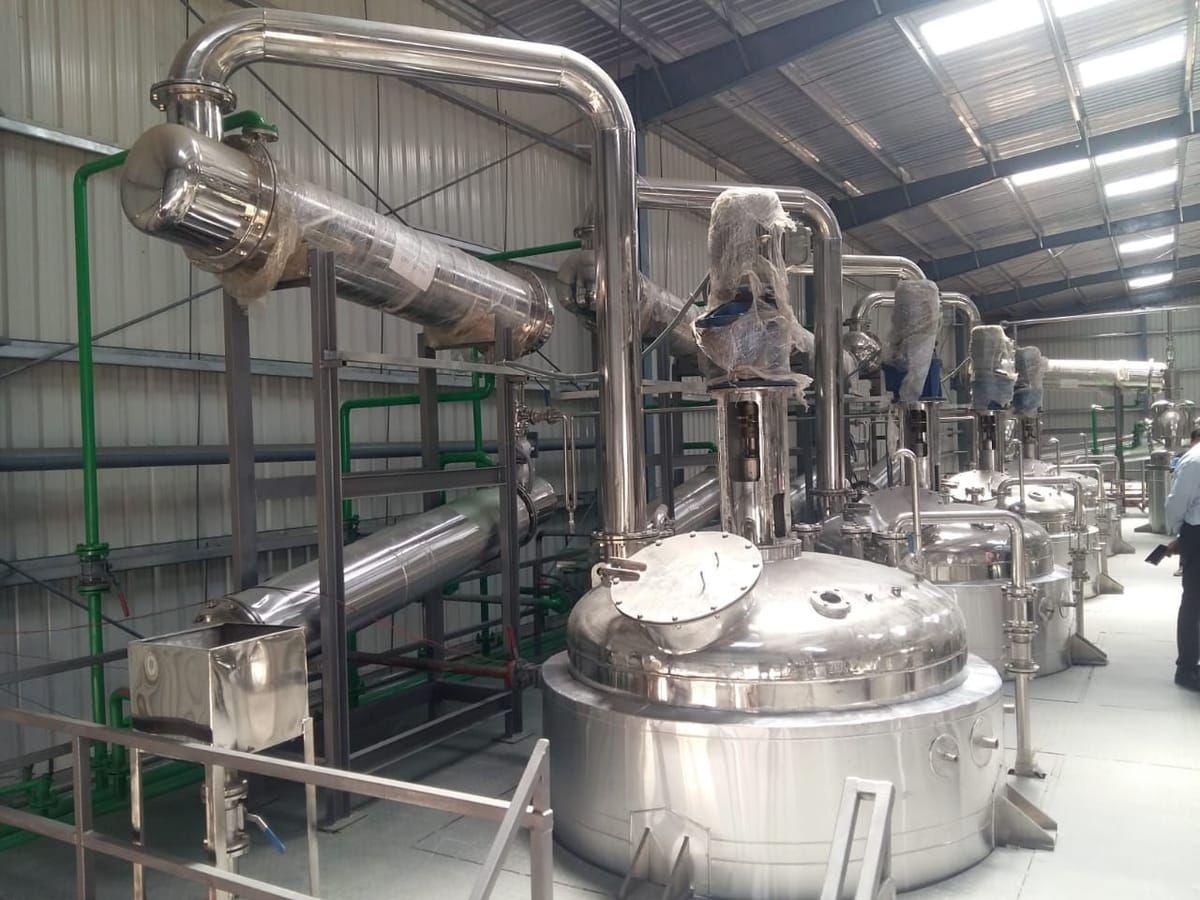
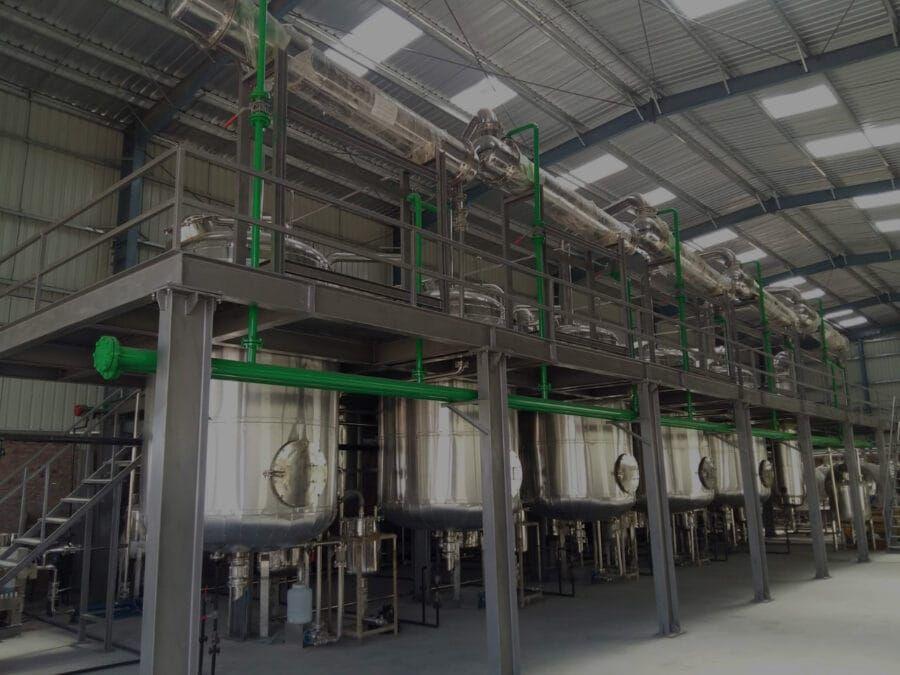
- Stainless Steel Solvent Extractors
- Miscella Holding Tanks
- Vacuum Evaporators
- Closed-Loop Solvent Recovery System
- Concrete Collection Tanks
- Ethanol Dissolution Tanks
- Chilling System
- Wax Separation Filters
- Vacuum Concentrators
- Absolute Storage Tanks
- PLC-SCADA Automation System
- Electrical MCC
- Instrumentation Package
- Automatic CIP System
Automation Features
The intelligent PLC-SCADA platform includes:
- Automatic Recipe Management
- Solvent Flow Control
- Vacuum Control
- Temperature Monitoring
- Solvent Recovery Monitoring
- Batch Traceability
- Alarm Management
- Utility Monitoring
- Production Analytics
- Remote Diagnostics
- Predictive Maintenance
- Industry 4.0 Integration
GMP & Safety Features
The facility is designed with hygienic, GMP-oriented practice in view; the standards that apply to the client's facility and product are scoped per project. Features include:
- SS 316L product-contact surfaces
- Closed-loop solvent handling
- ATEX-compatible explosion-proof design (optional)
- Hygienic sanitary piping
- Automatic CIP cleaning
- Validation-ready engineering
- GMP-oriented layout
- HACCP-oriented design
- Cross-contamination prevention
Plant Utilities
- Steam Boiler
- Thermic Fluid Heater
- Chilling Plant
- Cooling Tower
- Vacuum System
- Air Compressor
- RO Water System
- Nitrogen Blanketing System
- Electrical Power
Sustainability Features
The plant incorporates environmentally responsible engineering through:
- Closed-loop solvent recycling
- Closed-loop solvent recovery
- Low VOC emissions
- Heat recovery from vacuum systems
- Utility optimisation
- Reduced environmental impact
- Energy-efficient processing
Customer Benefits
Following successful commissioning, the customer achieved:
- Higher fragrance recovery
- Reduced solvent consumption
- Designed for efficient operation
- Improved production consistency
- Increased manufacturing capacity
- Enhanced export competitiveness
- Reduced environmental footprint
Plants Used In This Project
Why Mechotech?
Mechotech is a manufacturer of turnkey botanical extraction plants, solvent extraction systems, essential oil processing plants, nutraceutical machinery, pharmaceutical process equipment, and fragrance ingredient manufacturing facilities. With engineering excellence, we deliver advanced solvent extraction technologies, intelligent PLC-SCADA automation, GMP-oriented engineering, and sustainable processing solutions for the world's most valuable botanical products.
Conclusion
The Tuberose Absolute Extraction Plant from Mechotech provides a complete turnkey solution for manufacturing premium Tuberose Concrete and Tuberose Absolute. Through advanced closed-loop solvent extraction, high-efficiency solvent recovery, vacuum purification, intelligent automation, and GMP-oriented engineering, the facility combines these process stages in a single turnkey solution.
Key Technical Highlights
- Raw Material
- Agave amica (Polianthes tuberosa)
- Finished Products
- Tuberose Concrete, Tuberose Absolute
- Technology
- Closed-Loop Solvent Extraction + Vacuum Solvent Recovery + Ethanol Purification + Chilled Filtration
- Automation
- PLC-SCADA with Industry 4.0 Integration
- Construction Material
- SS 304 / SS 316L
- Solvent Recovery
- Established during process development
- Compliance
- Hygienic, GMP-oriented design with documentation to support the client's qualification; applicable standards are scoped per project
- Applications
- Luxury Perfumery, Cosmetics, Pharmaceuticals, Aromatherapy, Personal Care
Why Global Manufacturers Choose Mechotech
- engineering excellence in floral extraction and solvent recovery technologies
- Complete turnkey solutions from 100 kg/day pilot plants to industrial facilities
- Advanced closed-loop solvent extraction
- Intelligent PLC-SCADA automation with complete production traceability
- GMP-oriented hygienic and explosion-safe engineering
- Energy-efficient vacuum evaporation and utility optimisation
- Complete installation, commissioning, validation, operator training, preventive maintenance, spare parts supply, and lifetime technical support
- Proven expertise in essential oils, floral absolutes, herbal extracts, oleoresins, phytochemicals, nutraceuticals, pharmaceutical process plants, and premium fragrance ingredient manufacturing
Planning a Similar Plant?
Mechotech engineers are ready to assess your process and design the right plant for your target output.
Get a Free Consultation