Executive Summary
A manufacturer of botanical ingredients required a fully automated, GMP-oriented Clove Essential Oil Distillation Plant to manufacture premium-quality Clove Essential Oil, Eugenol-Rich Oil, and specialty essential oil fractions for pharmaceutical, food, flavour, fragrance, cosmetic, and dental care industries.
The customer required a turnkey solution capable of maximising essential oil recovery, preserving natural eugenol content, minimising steam consumption, reducing processing time, and consistently producing export-grade oil compliant with international quality standards.
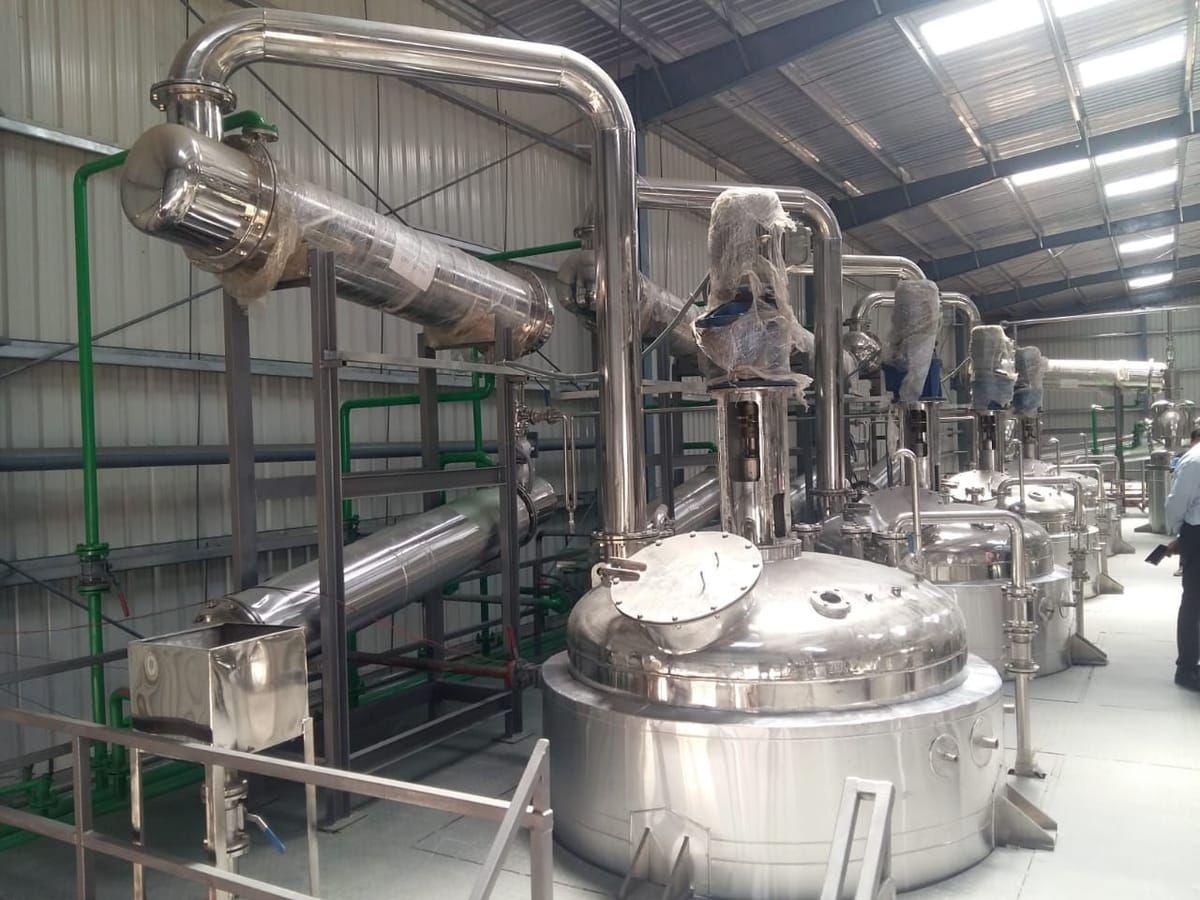
Mechotech successfully designed, engineered, manufactured, installed, and commissioned a Clove Essential Oil Distillation Plant incorporating advanced steam distillation, precision condensation, oil-water separation, condensate recovery, automated utility management, and intelligent PLC-SCADA automation.
Customer Background
The customer manufactures natural essential oils for pharmaceutical companies, dental care manufacturers, flavour & fragrance industries, food ingredient companies, cosmetic manufacturers, personal care brands, aromatherapy companies, and global essential oil exporters. With growing worldwide demand for natural Clove Oil and Eugenol, the customer required a modern, energy-efficient facility capable of continuous high-quality production.
Customer Challenges
Before modernisation, the customer experienced:
- Low oil recovery
- Inconsistent eugenol concentration
- High steam consumption
- Long batch cycles
- Manual operation
- Variable product quality
- High operating costs
- Limited production capacity
- Difficulty meeting international export standards
Project Objectives
Mechotech developed a turnkey solution capable of:
- Processing 15 MT/day of Clove Buds
- Maximising essential oil recovery
- Producing high-eugenol oil
- Reducing utility consumption
- Improving production consistency
- Documentation to support the customer's quality and regulatory qualification
- Supporting expansion
Raw Material
- Botanical Name
- Syzygium aromaticum
- Common Name
- Clove
- Plant Part Used
- Dried Flower Buds
- Moisture Content
- 8–10%
- Daily Processing Capacity
- 15,000 kg/day
Finished Product
Available Options
Applications
- Pharmaceuticals
- Dental Preparations
- Oral Care Products
- Flavour Manufacturing
- Food Processing
- Cosmetics
- Aromatherapy
- Personal Care Products
Process Flow
Process Description
Raw Material Preparation
Premium-quality dried clove buds are cleaned and inspected before loading into stainless steel distillation vessels. Depending on customer requirements, cloves may be lightly crushed to improve oil release without affecting oil quality.
Steam Distillation
Steam generated in a high-efficiency boiler passes uniformly through the clove bed, extracting volatile essential oil compounds.
The process ensures:
- High eugenol preservation
- Uniform steam distribution
- Reduced processing time
- Consistent product quality
Condensation
Oil-laden vapours are condensed using high-efficiency shell-and-tube condensers designed for rapid heat transfer.
Benefits include:
- Efficient condensation
- Lower oil losses
- Reduced cooling water consumption
- Stable plant operation
Oil-Water Separation
Condensed liquid enters precision-engineered Florentine separators where Clove Essential Oil is separated from hydrosol.
Recovered products include:
- Premium Clove Essential Oil
- Clove Hydrosol (optional value-added product)
Oil Filtration
The separated oil passes through micron filtration systems to achieve excellent clarity while preserving natural aroma and active compounds.
Quality Standardisation
Each production batch is tested for:
- Eugenol Content
- Specific Gravity
- Refractive Index
- Optical Rotation
- Colour
- Moisture
- Purity
- Organoleptic Properties
Only batches meeting customer specifications proceed to packaging.
Major Equipment Supplied
- Raw Material Cleaning System
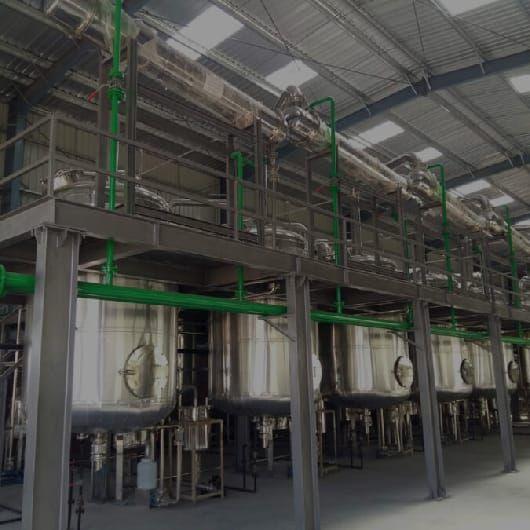
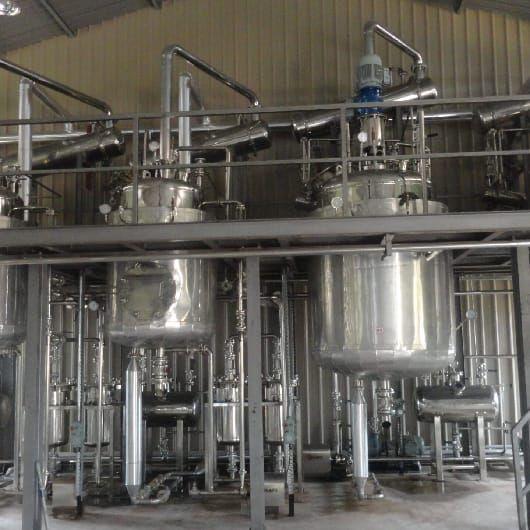
- Stainless Steel Steam Distillation Vessels
- Steam Distribution System
- High-Efficiency Boiler
- Shell & Tube Condensers
- Florentine Oil Separators
- Oil Filtration System
- Essential Oil Storage Tanks
- Hydrosol Collection Tanks
- Cooling Tower
- Transfer Pumps
- PLC-SCADA Automation Panel
- Electrical MCC
- Instrumentation Package
- CIP System
Automation Features
The plant incorporates advanced automation including:
- Automatic Steam Flow Control
- Distillation Recipe Management
- Temperature Monitoring
- Pressure Monitoring
- Cooling Water Control
- Batch Timing Automation
- Alarm Management
- Historical Batch Records
- Utility Monitoring
- Production Reporting
- Remote Diagnostics
- Industry 4.0 Connectivity
GMP & Safety Features
The facility is designed with hygienic, GMP-oriented practice in view; the standards that apply to the client's facility and product are scoped per project. Features include:
- SS 316L product-contact surfaces
- Hygienic piping systems
- CIP-compatible construction
- Food-grade seals and gaskets
- Dead-leg-free process design
- Automated cleaning systems
- Validation-ready equipment
- GMP-oriented layout
- HACCP-oriented manufacturing
Plant Utilities
- Steam Boiler
- Cooling Tower
- Soft Water System
- Air Compressor
- Electrical Power
- Instrument Air
- Process Water
Sustainability Features
The plant incorporates sustainable engineering through:
- Condensate recovery and reuse
- Heat recovery systems
- Optimised steam utilisation
- Water recycling
- Energy-efficient condensers
- Reduced emissions
- Automated utility optimisation
- Eco-friendly process engineering
Customer Benefits
Following successful commissioning, the customer achieved:
- Increased oil recovery
- Higher eugenol retention
- Reduced steam consumption
- Designed for efficient operation
- Increased production capacity
- Better process control
- Enhanced product stability
- Improved customer satisfaction
- Strong return on investment
Plants Used In This Project
Why Mechotech?
Mechotech is a manufacturer of turnkey extraction and distillation plants for essential oils, herbal extracts, nutraceuticals, pharmaceuticals, spice processing, and food ingredient industries. Our expertise in steam distillation, hydro-distillation, condensate recovery, intelligent automation, and GMP-oriented engineering enables customers worldwide to manufacture premium essential oils.
Conclusion
The Clove Essential Oil Distillation Plant from Mechotech delivers a complete turnkey solution for producing premium Clove Essential Oil with high eugenol content. By integrating advanced steam distillation technology, intelligent automation, energy-efficient utilities, and hygienic GMP engineering, the facility combines these process stages in a single turnkey solution.
Key Technical Highlights
- Raw Material
- Syzygium aromaticum (Clove Buds)
- Finished Products
- Clove Essential Oil, Eugenol-Rich Oil, Clove Hydrosol
- Distillation Technology
- Steam Distillation / Hydro-Distillation (Optional)
- Automation
- PLC-SCADA with Industry 4.0 Integration
- Construction Material
- SS 304 / SS 316L
- Compliance
- Hygienic, GMP-oriented design with documentation to support the client's qualification; applicable standards are scoped per project
- Applications
- Pharmaceuticals, Dental Care, Food Ingredients, Flavour & Fragrance, Cosmetics, Aromatherapy
Why Global Manufacturers Choose Mechotech
- process engineering excellence
- Complete turnkey project execution from feasibility study to commissioning
- Pilot plants through industrial facilities
- High-efficiency steam distillation with optimised utility consumption
- Precision condensers and high-performance oil separation systems
- PLC-SCADA automation with batch traceability and production analytics
- Hygienic, GMP-oriented design with documentation to support the client's qualification; applicable standards are scoped per project
- Comprehensive installation, validation, operator training, annual maintenance support, and lifetime technical assistance
- Proven expertise in essential oils, spice processing, herbal extraction, nutraceuticals, pharmaceuticals, and food processing technologies
Planning a Similar Plant?
Mechotech engineers are ready to assess your process and design the right plant for your target output.
Get a Free Consultation