Executive Summary
A botanical ingredient manufacturer required a fully automated, GMP-oriented Licorice (Glycyrrhizin) Extraction Plant capable of manufacturing premium Glycyrrhizin Extract, Deglycyrrhizinated Licorice (DGL), Licorice Root Extract, and standardised botanical ingredients for global pharmaceutical, nutraceutical, food, and cosmetic industries.
The customer required a turnkey processing facility capable of maximising glycyrrhizin recovery, preserving flavonoids and triterpenoid saponins, minimising solvent and utility consumption, and consistently producing export-grade products to the customer's quality and regulatory requirements, with documentation to support qualification.
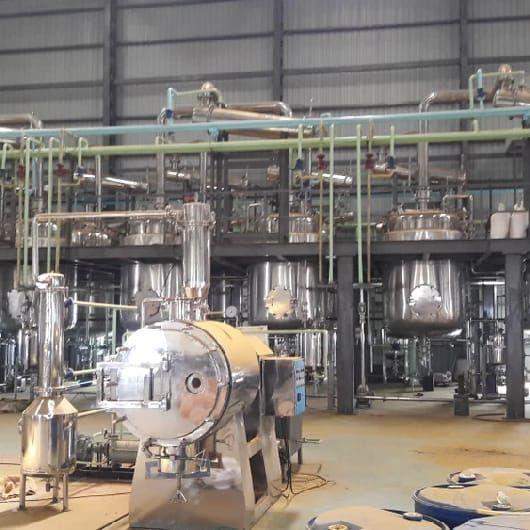
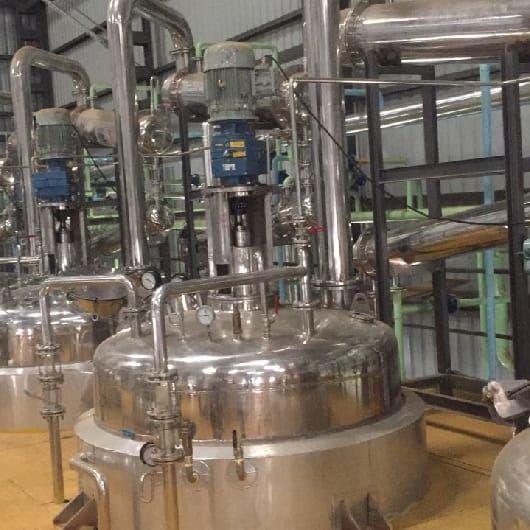
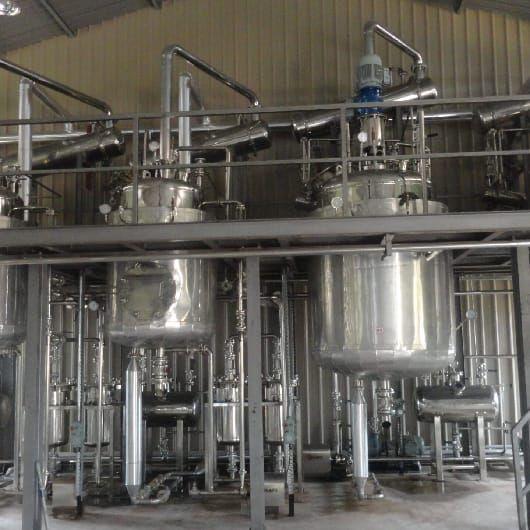
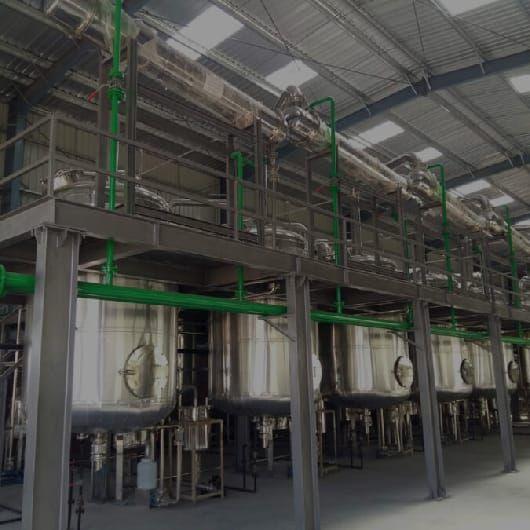
Mechotech successfully designed, engineered, manufactured, supplied, installed, and commissioned a Licorice Extraction Plant integrating advanced raw material preparation, hydro-alcoholic extraction, membrane clarification, solvent recovery, purification, concentration, spray drying, and intelligent PLC-SCADA automation.
Customer Background
The customer manufactures botanical ingredients for pharmaceutical companies, nutraceutical manufacturers, herbal medicine companies, functional food manufacturers, cosmetic companies, food ingredient producers, veterinary product manufacturers, and international botanical ingredient exporters. Growing worldwide demand for natural anti-inflammatory, digestive health, respiratory wellness, and cosmetic ingredients encouraged investment in a modern automated extraction facility.
Customer Challenges
Before modernisation, the customer experienced:
- Low glycyrrhizin recovery
- Variable active compound concentration
- High solvent consumption
- Inconsistent extraction efficiency
- Long production cycles
- Manual process variability
- High utility costs
- Limited production capacity
- Difficulty meeting export specifications
Project Objectives
Mechotech developed a turnkey solution capable of:
- Processing 20 MT/day of Licorice Roots
- Producing standardised Glycyrrhizin Extract
- Manufacturing Deglycyrrhizinated Licorice (DGL)
- Recovering extraction solvent for reuse
- Preserving bioactive flavonoids
- Reducing utility consumption
- Documentation to support the customer's quality and regulatory qualification
- Supporting future expansion
Raw Material
- Botanical Name
- Glycyrrhiza glabra
- Common Name
- Licorice
- Plant Part Used
- Roots
- Major Bioactive Compounds
- Glycyrrhizin, Glycyrrhetinic Acid, Liquiritin, Isoliquiritigenin, Glabridin, Flavonoids
- Daily Processing Capacity
- 20,000 kg/day
Finished Product
Available Options
Applications
- Digestive Health Supplements
- Respiratory Health Products
- Anti-inflammatory Formulations
- Herbal Medicines
- Functional Foods
- Cosmetics
- Oral Care Products
- Pharmaceutical Preparations
Process Flow
Process Description
Raw Material Preparation
Premium-quality Licorice roots are cleaned, inspected, cut, and milled into a controlled particle size to maximise extraction efficiency and improve solvent penetration.
Hydro-Alcoholic Extraction
Prepared Licorice root is extracted using pharmaceutical-grade hydro-alcoholic solvents under carefully controlled operating conditions.
The extraction process provides:
- High glycyrrhizin recovery
- Reduced degradation
- Uniform extraction
- Consistent product quality
Filtration
The crude extract passes through pressure filtration systems to remove insoluble plant materials before concentration.
Vacuum Solvent Recovery
The filtered extract enters high-efficiency vacuum evaporators where solvent is recovered, condensed, purified, and reused.
Benefits include:
- Designed for efficient operation
- Enhanced environmental performance
- Improved plant safety
Vacuum Concentration
The extract is concentrated under vacuum at low temperatures to preserve sensitive phytochemicals and antioxidant activity.
Membrane Purification
Microfiltration and ultrafiltration systems improve product purity by removing suspended solids and undesirable impurities.
Advantages include:
- Higher purity
- Better colour
- Improved stability
- Lower processing losses
Resin Purification
Specialised adsorption resin columns selectively enrich glycyrrhizin while removing unwanted compounds.
This stage provides:
- High active content
- Better product appearance
- Pharmaceutical-grade quality
Standardisation
Finished extract is standardised according to customer specifications. Typical standardisations include:
- Glycyrrhizin
- Glycyrrhetinic Acid
- Glabridin
- Flavonoids
- Moisture
- Bulk Density
- Particle Size
For DGL production, controlled downstream processing reduces glycyrrhizin content while preserving beneficial flavonoids.
Spray Drying
The standardised extract is spray dried into a free-flowing powder suitable for capsule, tablet, beverage, and functional food applications.
Quality Standardisation
Each production batch is analysed for:
- Glycyrrhizin
- Glycyrrhetinic Acid
- Glabridin
- Total Flavonoids
- Moisture
- Residual Solvent
- Heavy Metals
- Pesticide Residues
- Microbial Limits
- Particle Size
- Bulk Density
Major Equipment Supplied
- Raw Material Cleaning System
- Root Cutting Machine
- Hammer Mill
- Stainless Steel Extraction Vessels
- Solvent Storage Tanks
- Pressure Leaf Filters
- Vacuum Evaporators
- Solvent Recovery System
- Microfiltration System
- Ultrafiltration System
- Resin Purification Columns
- Spray Dryer
- Ribbon Blender
- Product Storage Silos
- PLC-SCADA Automation Panel
- Electrical MCC
- Instrumentation Package
- CIP/SIP System
Automation Features
The plant incorporates advanced PLC-SCADA automation including:
- Recipe Management
- Automatic Extraction Sequencing
- Temperature Monitoring
- Solvent Flow Monitoring
- Vacuum Control
- Membrane Monitoring
- Resin Column Automation
- Spray Dryer Control
- Batch Traceability
- Alarm Management
- Production Analytics
- Utility Monitoring
- Remote Diagnostics
- Industry 4.0 Connectivity
GMP & Safety Features
The facility is designed with hygienic, GMP-oriented practice in view; the standards that apply to the client's facility and product are scoped per project. Features include:
- SS 316L product-contact surfaces
- Hygienic sanitary piping
- Closed-loop solvent extraction
- Explosion-proof electrical systems
- Nitrogen blanketing
- Food & pharmaceutical-grade elastomers
- CIP & SIP compatible systems
- Validation-ready construction
- GMP-oriented layout
- HACCP-oriented engineering
Plant Utilities
- Steam Boiler
- Cooling Tower
- Chilled Water System
- Vacuum System
- Air Compressor
- RO Water System
- Soft Water System
- Electrical Power
- Nitrogen Supply
Sustainability Features
The plant incorporates environmentally responsible engineering through:
- Closed-loop solvent recovery
- Heat recovery systems
- Low-energy vacuum concentration
- Water conservation systems
- Utility optimisation
- Reduced emissions
- Sustainable extraction technology
- Eco-friendly manufacturing practices
Customer Benefits
Following successful commissioning, the customer achieved:
- Higher glycyrrhizin recovery
- Improved extract purity
- Closed-loop solvent recovery
- Designed for efficient operation
- Reduced utility consumption
- Increased manufacturing capacity
- Consistent pharmaceutical-grade quality
- Enhanced export competitiveness
Plants Used In This Project
Why Mechotech?
Mechotech is a manufacturer of turnkey extraction plants for nutraceuticals, pharmaceuticals, herbal extracts, natural ingredients, essential oils, and specialty botanical products. With engineering expertise, our advanced extraction technologies, membrane purification systems, solvent recovery solutions, adsorption technologies, and PLC-SCADA automation enable customers worldwide to manufacture premium botanical ingredients.
Conclusion
The Licorice (Glycyrrhizin) Extraction Plant from Mechotech provides a complete turnkey solution for manufacturing premium Glycyrrhizin Extract, Deglycyrrhizinated Licorice (DGL), and standardised Licorice Root Extracts. Through advanced extraction, membrane purification, intelligent automation, and GMP-oriented engineering, the facility combines these process stages in a single turnkey solution.
Key Technical Highlights
- Raw Material
- Glycyrrhiza glabra (Licorice Root)
- Finished Products
- Glycyrrhizin Extract, DGL, Licorice Root Extract, Pharmaceutical-Grade Botanical Ingredients
- Technology
- Hydro-Alcoholic Extraction + Membrane Filtration + Resin Purification + Spray Drying
- Solvent Recovery
- Established during process development
- Automation
- PLC-SCADA with Industry 4.0 Integration
- Construction Material
- SS 304 / SS 316L
- Compliance
- Hygienic, GMP-oriented design with documentation to support the client's qualification; applicable standards are scoped per project
- Applications
- Pharmaceuticals, Nutraceuticals, Functional Foods, Cosmetics, Herbal Medicines, Food Ingredients
Why Global Manufacturers Choose Mechotech
- engineering excellence in botanical extraction and pharmaceutical process engineering
- Complete turnkey execution from laboratory development to commercial production
- Customised plants from 100 kg/day pilot systems to industrial facilities
- Advanced extraction, membrane separation, purification, and standardisation technologies
- Intelligent PLC-SCADA automation with complete batch traceability
- High-efficiency solvent recovery systems
- Hygienic, GMP-oriented design with documentation to support the client's qualification; applicable standards are scoped per project
- Comprehensive installation, validation, operator training, preventive maintenance, spare parts support, and lifetime technical assistance
- Proven expertise in herbal extracts, nutraceuticals, pharmaceuticals, natural colours, essential oils, oleoresins, and specialty botanical processing plants
Planning a Similar Plant?
Mechotech engineers are ready to assess your process and design the right plant for your target output.
Get a Free Consultation