Anise Seeds
Anise Seeds
Mechotech designs and manufactures turnkey seeds & berries distillation plants for Anise Seeds. We supply the complete machinery to process Anise Seeds into an essential oil configured to the client’s target specification for the pharmaceutical, nutraceutical, food, and fragrance industries. Anise (Pimpinella anisum) oil is dominated by trans-anethole (typically 80–95%), the compound behind its sweet, liquorice-like aroma, and is a key flavouring in anise liqueurs (Pastis, Arak, Ouzo), confectionery and over-the-counter expectorant medicines.
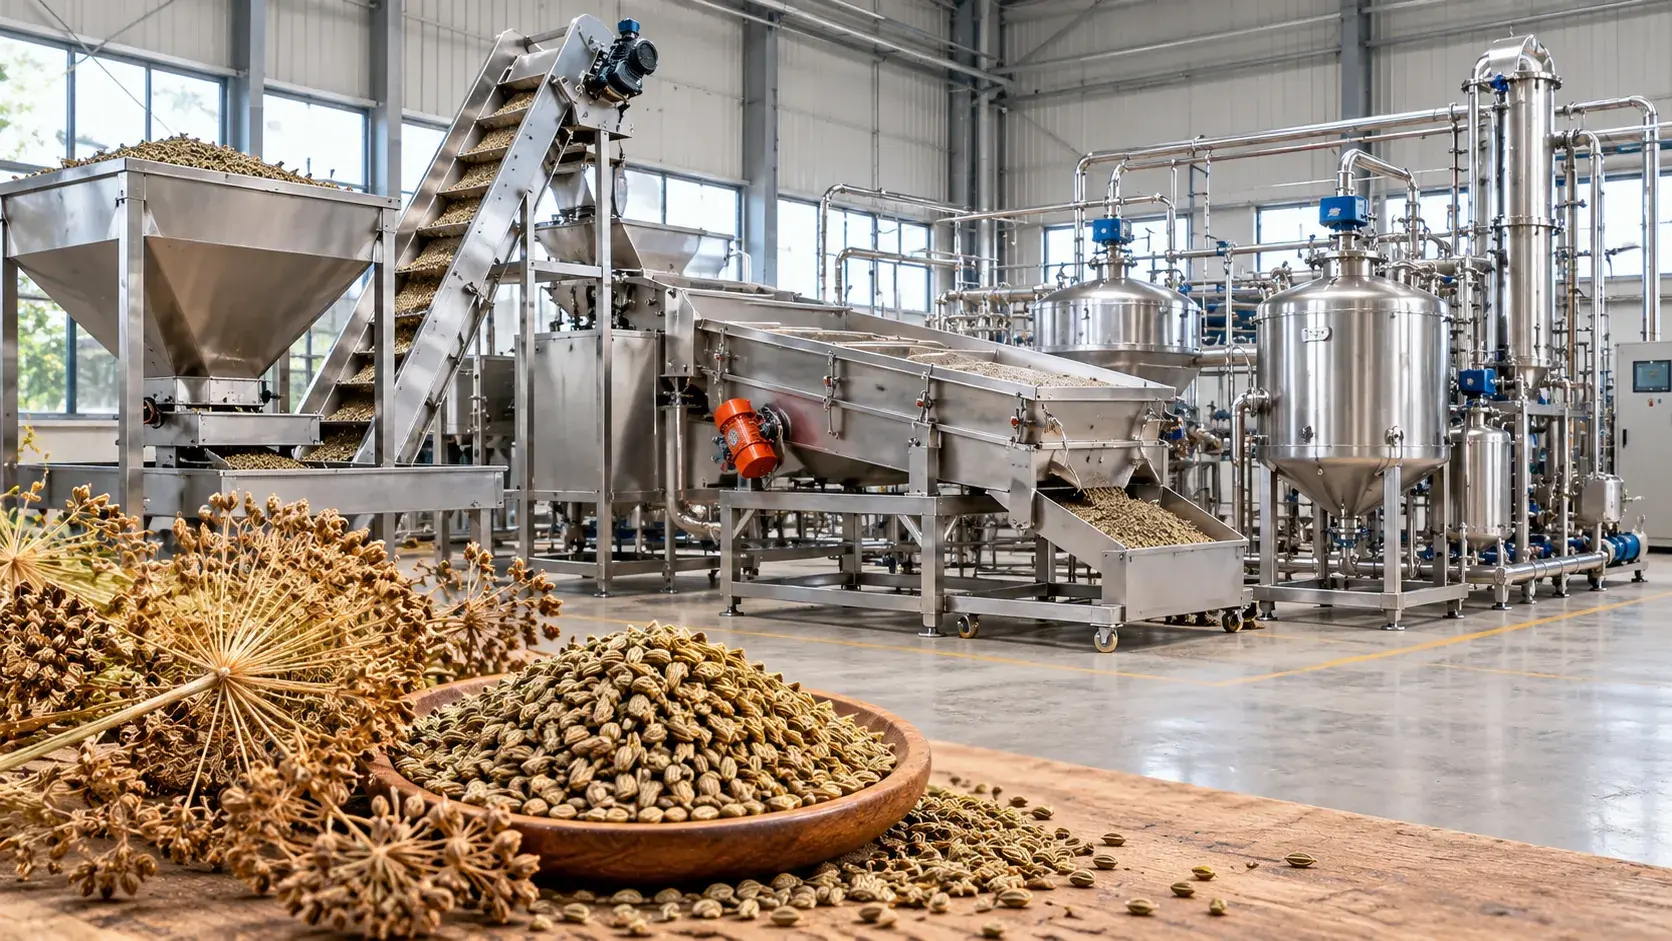
Mechotech's Anise Seeds plant is configured around the specific chemistry and processing requirements of Anise Seeds. Built in SS 316L with integrated condensers and oil-water separation, PLC-based automation, and full documentation, each plant is delivered as a commissioned turnkey system. Anise is a small, aromatic seed, so the line is built around cleaning and lightly crushing the seed shortly before charging; trans-anethole is the characteristic constituent of the oil.
Technical Specifications
| Product | Anise Seeds Distillation Plant |
|---|---|
| Botanical Name | Pimpinella anisum |
| Process Category | Seeds & Berries Distillation Plants |
| Plant Part | Seeds |
| Extract Type | Essential oil, with aromatic hydrosol as a recoverable co-product |
| Extraction Method | Steam, hydro (hydrodistillation), vacuum or pressure distillation — selected for the volatility and heat-sensitivity of the target oil |
| Product-contact Material | SS 316L, CIP-capable |
| Condensation & Separation | Multi-tube condenser with chilled-water circulation; stainless-steel Florentine flask for oil–water separation |
| Polishing | Polish filtration; drying over anhydrous sodium sulphate or by vacuum |
| Quality Control | GC-MS and physical parameters (specific gravity, refractive index, optical rotation) verified per batch |
| Utility Requirements | Steam, chilled/cooling water, compressed air, soft water, power (project-specific) |
| Automation | PLC-based automation |
| Plant Capacity | Configured to requirement |
| Final Product Form | Essential oil (liquid) and recoverable hydrosol |
Plant Capacities
| Plant Scale | Raw Material Throughput | Typical Use |
|---|---|---|
| Pilot | Configured to your feedstock and trial plan | Product development, parameter validation |
| Semi-Commercial | Configured between pilot and commercial scale | Contract manufacturing, scale-up trials |
| Commercial | Configured to raw-material supply and confirmed buyer volume | Commercial production at confirmed buyer volume |
Capacity is configured to raw-material supply and confirmed buyer volume; we recommend a pilot plant to validate process parameters before scaling.
Manufacturing Process
Raw Material Preparation
Anise (Pimpinella anisum) seed is cleaned and lightly crushed shortly before charging so that steam reaches the oil held in the seed; the crushing degree and charge density are set during process development.
Charging & Distillation
The prepared Anise Seeds charge is loaded into the SS 316L still and distilled by steam, hydro (hydrodistillation), vacuum, or pressure distillation — selected for the volatility and heat-sensitivity of the target oil.
Condensation
Vapours pass through an efficient multi-tube condenser with chilled-water circulation, condensing the volatile oil and hydrosol.
Oil–Water Separation
Condensate is separated in a stainless-steel Florentine flask; the essential oil is collected while the hydrosol is drawn off (and can be recovered as a co-product).
Polishing & Drying
The crude oil is polish-filtered and dried over anhydrous sodium sulphate (or by vacuum) to remove residual moisture.
Quality Control
Each batch of Anise Seeds oil is verified by GC-MS and physical parameters (specific gravity, refractive index, optical rotation) before release.
Major Plant Equipment
- Raw material cleaning and sorting (with size reduction where required)
- SS 316L distillation still
- Steam distribution system
- Multi-tube condenser (chilled-water circulation)
- Stainless-steel Florentine oil–water separator
- Polish filtration and drying unit (anhydrous sodium sulphate or vacuum)
- Hydrosol collection
- Essential oil and hydrosol storage tanks
- CIP (clean-in-place) system
- PLC-based automation panel
Plant Output
Applications
- Anise liqueur flavouring (Pastis, Arak, Ouzo)
- Confectionery flavouring
- Over-the-counter expectorant medicines
Key Features
SS 316L Construction
All product-contact surfaces are SS 316L for corrosion resistance and product purity, with CIP capability between batches.
Efficient Condensation
High-surface-area multi-tube condensers with chilled-water circulation maximise oil recovery and minimise losses of volatile top-notes.
Seed-Charge Distillation
The still is configured for dense, lightly crushed seed charges, with the distillation mode set during process development.
Hydrosol Recovery
Integrated separation allows recovery of the aromatic hydrosol as a co-product.
Scalable Capacity
Plants are configured to requirement from pilot scale upward, with modular expansion.
Frequently Asked Questions
Does Mechotech supply the complete machinery for Anise Seeds?
What specification can the Anise Seeds plant achieve?
What production capacities are available for the Anise Seeds plant?
Which industries use the Anise Seeds plant?
How is Anise Seeds essential oil produced in Mechotech's distillation plant?
Has Mechotech delivered a distillation plant on a similar feedstock to Anise Seeds?
Ready to discuss your project?
Get a free quote and technical consultation from our engineering team.